China remains one of the world’s most important manufacturing bases, offering buyers access to a broad range of products, production capabilities, and competitive supply chains. However, finding a supplier is relatively easy. Determining whether that supplier can consistently manufacture the right product, at the required quality level and on schedule, is more difficult.
Effective supplier selection in China therefore requires more than comparing quotations. Buyers should verify the supplier’s identity, manufacturing capability, quality control system, production capacity, and ability to meet specific product requirements before placing significant orders.
1. Verify the Supplier Before Placing an Order
The first step is confirming who you are actually dealing with.
A supplier may operate as a manufacturer, trading company, sourcing company, or a combination of these. This does not automatically determine whether the supplier is suitable, but buyers should understand the business relationship before making payments or committing to production.
Basic verification should include the company’s registered name, business license, registered address, factory location, contact information, and whether the company presented to the buyer matches the actual manufacturing facility.
A supplier verification can provide an independent on-site check when a buyer needs basic confirmation of a potential supplier before proceeding further.
2. Assess Actual Manufacturing Capability
A professional website, product catalogue, or showroom does not necessarily demonstrate manufacturing capability.
Buyers should determine whether the factory has suitable machinery, production processes, workforce, technical experience, and capacity for the intended product.
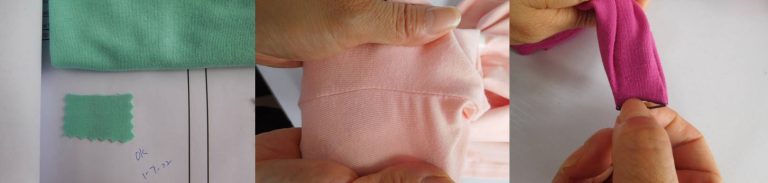
For example, an apparel buyer may need to review cutting, sewing, finishing, ironing, needle detection, and packing capabilities. A buyer sourcing mechanical products may focus more heavily on machining equipment, assembly processes, testing facilities, measuring instruments, and technical personnel.
A factory audit can help verify whether the supplier’s actual facilities and production resources are consistent with what has been presented during the sourcing process.
3. Review the Factory’s Quality Control System
Production capability alone is not enough. A factory also needs an effective method for controlling quality.
Buyers should look at how incoming materials are checked, how production defects are identified, whether finished products are inspected, how non-conforming goods are handled, and whether quality records are properly maintained.
The sophistication of the system will vary significantly between industries and factories. What matters is whether the controls are appropriate for the product and whether they are actually implemented in daily production.
For long-term suppliers, periodic factory audits can also help buyers monitor changes in production conditions, staffing, equipment, documentation, and quality management.
4. Check Product-Specific Compliance Requirements
Certifications should be evaluated according to the product and destination market rather than treated as a general supplier qualification.
Different products may be subject to different regulatory, safety, labeling, testing, or documentation requirements. An electrical product, toy, garment, furniture item, or industrial component may have very different compliance obligations.
Buyers should identify the applicable requirements before production and confirm which party is responsible for testing, certification, technical documentation, and labeling.
Where certificates or test reports are required, their validity, product coverage, issuing organization, and relationship to the actual goods should also be checked.
5. Evaluate Samples, Specifications, and Communication
A supplier cannot reliably meet requirements that have not been clearly defined.
Before mass production, buyers should establish reference documents such as approved samples, specifications, drawings, tech packs, artwork, color standards, packaging instructions, and labeling requirements.
It is also useful to evaluate how the supplier responds when requirements change or problems are identified. Fast and accurate communication during sampling often provides useful insight into how the supplier may perform during bulk production.
The goal is not simply to find a factory capable of producing the product, but one capable of consistently following the buyer’s requirements.
6. Use Inspections During Production and Before Shipment
Supplier approval should not eliminate the need for product inspection.
Even an established supplier can experience material changes, production errors, workmanship defects, incorrect labeling, packaging problems, or quantity discrepancies.
A During Production Inspection can identify issues while production is still underway, allowing corrective action before the full order is completed.
A Pre-Shipment Inspection is normally carried out when most or all goods have been completed. It can cover quantity, workmanship, dimensions, appearance, functionality, labeling, packaging, and other requirements according to the buyer’s specifications.
For higher-risk orders or strict quality requirements, buyers may also consider Full Inspection, where 100% of the goods are checked rather than relying only on statistical sampling.
Build Supplier Control Into the Procurement Process
Reliable sourcing is not based on a single audit or inspection. It is a process.
A practical supplier control strategy may include supplier verification before cooperation, a factory audit for important suppliers, clear product specifications before production, inspection during manufacturing when necessary, and final inspection before shipment.
NBNQC provides independent supplier verification, factory audit, quality control, and product inspection services across China, helping international buyers obtain clearer information about suppliers and production before making purchasing and shipment decisions.
Combining supplier assessment with ongoing product inspections gives buyers greater visibility into both the factory and the goods being produced—and helps identify quality risks before they become costly problems.